OEM Sandpaper Jumbo Rolls A Practical Buying Guide
2026-09-15
Most buying guides for OEM sandpaper jumbo rolls drown you in grit charts and roll weights. But if you've ever had a batch arrive with uneven coating or splices that snap under tension, you know those charts miss the real risks. This practical guide focuses on the overlooked details, from width tolerances to backing flexibility, so you can source with confidence. Along the way, we'll show how SHENZHEN SUN ABRASIVES tackles these pain points for buyers who need repeatable performance.
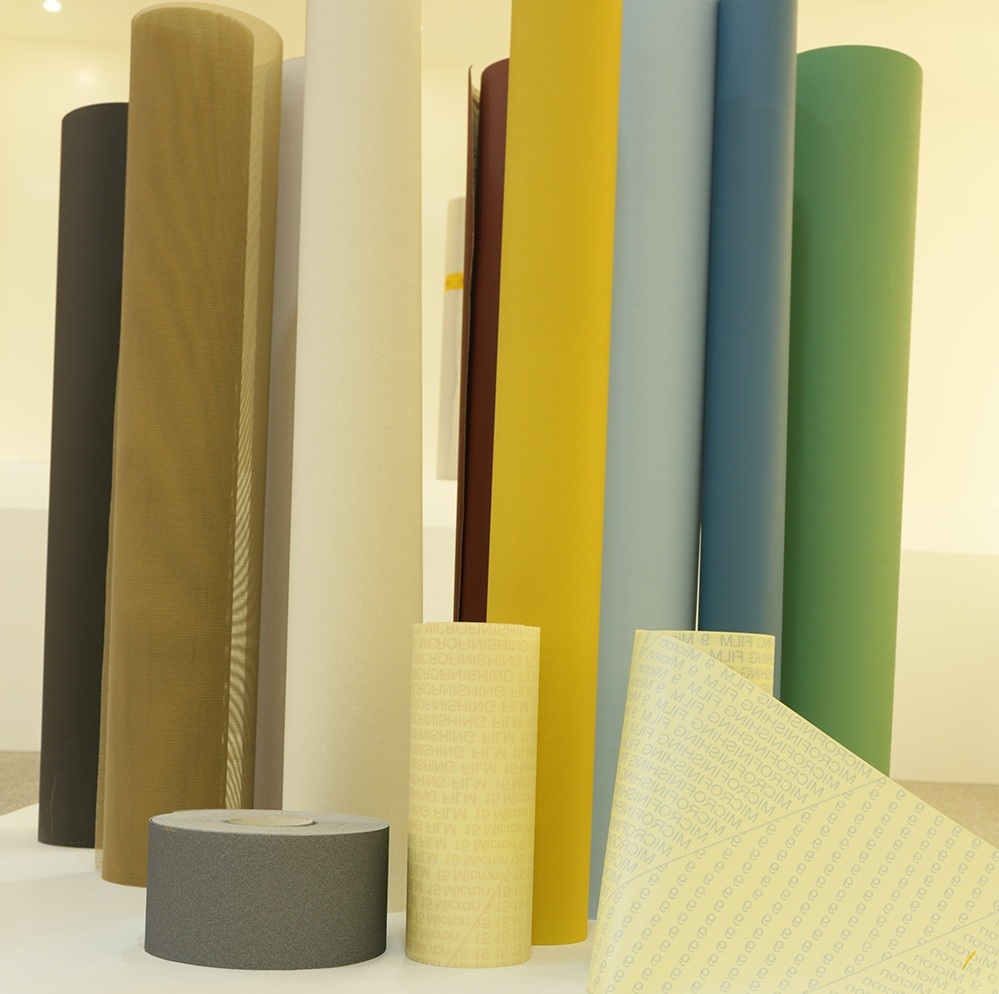
What Really Changes Between Paper, Cloth, and Film Backings?
The shift from paper to cloth isn't just about thickness. Paper will crease or snap once it's saturated or folded hard, while cloth tends to fray and tear only after serious abuse. That difference changes how long the abrasive lasts on edges and contours, not just how it feels in your hand.
Film sits in another spot altogether. Without the fiber grain that paper and cloth carry, the abrasive coating lays down with far fewer high spots. The result is a much more even scratch pattern on clear coats and metals, which is why film often shows up for fine finishing work where one stray deep scratch ruins the job.
So the real change comes down to how pressure, moisture, and flexing hit the backside. Paper gives up durability for low cost and flatness, cloth trades surface uniformity for toughness, and film sacrifices a little forgiveness in exchange for precision.
Why Grit Consistency Shows Up in Your Finish Quality
You can tell a lot about a finisher's grit by how smoothly the final coat levels out. The person who rushes through the sanding stages leaves faint scratches that only show up under a raking light, but the one who sticks with the process—going from 120 to 220 to 320 without skipping steps—gets that glass-smooth surface that catches light evenly. Consistency in the prep work translates directly into the quality of the finish, and that consistency comes from refusing to settle for “good enough.”
It's the same grit that shows up in the edges and corners. A determined finisher doesn't just hit the flat areas and call it done; they work the profiles and inside corners with the same patience, knowing that the eye is drawn to transitions first. Those details are where inconsistency becomes obvious, and where a steady hand and stubborn attention to detail pay off in a finish that looks professional from every angle.
At the end of the day, finish quality isn't about having the best tools or the most expensive materials—it's about the willingness to keep going when it's tedious, to redo a section that isn't right, and to hold the standard even when no one's watching. That's the grit that shows up in the final result, and it's the difference between a finish that looks good from across the room and one that looks good up close.
Getting Jumbo Roll Dimensions Right the First Time
Getting the dimensions right on a jumbo roll starts before a single sheet is wound. Too often, orders get placed using the nominal core size or an old spec sheet, only to find the roll won't fit the unwind stand or tears during converting. Take the time to measure the actual core inner diameter, wall thickness, and outer roll diameter under normal running conditions—not just on a sample bench. Even a 3 mm difference in core ID can cause chatter or slippage at high speeds.
Another overlooked factor is how the roll relaxes after winding. Fresh off the winder, a jumbo roll may measure true, but within a day it can sag or expand slightly depending on humidity and tension profile. If you need exact dimensions for a slitting or embossing line, record the roll at the same temperature and humidity where it will be used. Also check the end face for telescope or offset layers, which can throw off your diameter reading by several millimetres if you only measure one spot.
Finally, involve your converting team early. A quick call to the operator who loads the rolls can reveal whether a 76 mm core actually needs to be 76.2 mm to fit their air shaft, or whether the maximum outside diameter has to account for the guard clearance. These small clarifications, done before the purchase order, prevent expensive rework and downtime. Getting the dimensions right the first time is less about precision instruments and more about asking the right people the right questions.
When Custom Slitting Saves You Money (and When It Doesn't)
Custom slitting often pays off when your required widths don't match standard stock sizes. Buying pre-slit narrow coils usually comes with a markup for non-standard dimensions. Instead, purchasing full-width master rolls and having them slit to your exact specs means you pay only for the material you actually use, and you can combine several narrow widths from one master roll to cut down on leftover scrap. This approach works especially well if you regularly need a mix of widths that can be nested efficiently.
Another area where custom slitting saves money is inventory control. Keeping a smaller number of wide master rolls in stock and slitting them as orders come in reduces how much capital is tied up in finished goods. You avoid over-ordering specific narrow sizes that might sit on the shelf, and you can respond to demand changes without being stuck with obsolete inventory. For companies with fluctuating order patterns, that flexibility translates directly into lower carrying costs.
That said, custom slitting isn't automatically the cheaper route. If your volume is low, setup and changeover fees can easily eat up any material savings. When the width you need happens to be a common standard size, buying off-the-shelf narrow coils is usually less expensive because the slitting cost is already spread across large production runs. Short, frequent custom slitting jobs can also lead to more edge trim waste and downtime, since each new width requires stopping and adjusting the line.
Hidden Costs of Low-Priced Rolls You Should Know About
Low-priced rolls might look like a bargain on the shelf, but what you save upfront often comes back around in ways that are easy to overlook. For one, cheaper toilet paper tends to have fewer sheets per roll and thinner ply, which means you'll go through it much faster than you would with a mid-range or premium option. That forces more frequent trips to the store and more frequent replacement purchases, quietly erasing any initial savings within a week or two.
There's also the matter of how those rolls behave once they're actually in use. Low-cost paper often breaks apart too easily, leaving you grabbing extra sheets just to feel clean, or it clogs older plumbing systems because it doesn't dissolve as evenly. Plumbers' bills aren't cheap, and if you live in an older building, that “bargain” roll can turn into a costly repair call faster than you'd expect.
Beyond the practical side, there's the comfort factor that many people don't price into the equation. Rough, flimsy paper can lead to skin irritation, especially for anyone with sensitivities or for households with young children. Once you start adding up wasted sheets, extra store runs, potential plumbing fixes, and the discomfort of using something that barely does the job, that low sticker price stops looking like a deal and starts looking like a hidden tax on your daily routine.
Key Signs of a Reliable OEM Roll Supplier
Spotting a dependable OEM roll supplier often starts with how they handle dimensional consistency. You want to see repeated production runs where crown, diameter, and surface roughness stay within tight tolerances, not just on a sample report but across months of shipping records. Ask for actual inspection data from recent batches; if the supplier hesitates or only provides a generic certificate, that is usually a warning sign.
Another marker is their willingness to discuss failure modes before an order is placed. A solid supplier will bring up potential deflection under load, thermal expansion allowances, and coating adhesion risks without being prompted. They tend to ask detailed questions about your line speed, roll position, and maintenance intervals instead of immediately quoting a price. That kind of back-and-forth often separates experienced engineering partners from order takers.
Finally, watch how they handle post-delivery support. Reliable suppliers keep material traceability and heat-lot records for years, and they can usually send a technical person to walk your floor when a roll underperforms. If their default response is to blame the machine builder or the operator, the relationship may become costly later.
FAQ
Look beyond the grit number. A dependable roll keeps its bond intact under heat and pressure, has a consistent coating weight across the full width, and arrives with no wrinkles or telescoping. Ask the manufacturer how they monitor resin curing and whether they run continuous tension checks during slitting. If they hesitate on either point, treat that as a warning sign.
For metal, a heavy polyester or blended cloth backing holds up better to tearing and heat, while paper backings are usually fine for wood and painted surfaces where flexibility matters less. Cotton is cheap but stretches and can leave inconsistent scratch patterns. Match backing weight to the pressure your process applies—lighter isn't automatically worse, but it won't survive aggressive grinding.
Be precise about the material you're removing. Aluminum oxide works for most general jobs, but if you're grinding stainless steel or hard alloys, a ceramic or zirconia abrasive may reduce cost per part even at a higher roll price. Test one grit finer than you think you need—many buyers buy too coarse and then spend extra time refining the surface.
Ask for the full width tolerance, not just the nominal width. Request a roll hardness profile and the splice count per roll. Confirm the core size and whether the roll is wound face-in or face-out. Also ask for the coating weight in grams per square meter and a detailed cure curve. These details reveal whether the factory understands converting, not just coating.
Run a timed abrasion test on the actual surface you work with, not a generic test panel. Watch how quickly dust clears from the surface and whether edges fray within the first few minutes. Clogging is often tied to an under-cured resin or overly soft bond, while edge wear points to weak backing or uneven tension. Request a sample from the middle of a production run, not a hand-picked offcut.
Freight and handling are obvious, but many forget about core disposal, slitting waste, and import duties based on roll weight including packaging. Some suppliers quote a low square-meter price but then add charges for custom core sizes or moisture-resistant wrapping. Ask for a landed-cost breakdown per usable square meter, not per roll.
Give them the roll width, unwind direction, and any splice flags. If you're cutting pressure-sensitive adhesive discs, the liner release value matters more than the abrasive grit. Specify the exact disc diameter plus any center hole, and ask the converter to confirm they can hold tolerance across the full roll length. Misaligned splices or inconsistent release can stop a die-cutting line faster than a bad abrasive.
Test them blind on the same machine, same pressure, same surface, and same time interval. Measure weight loss on the workpiece, not just visual finish. Keep a reference sample from your current supplier, and run all candidates against it in the same shift—temperature and humidity change how abrasives cut. Also check the backing fingerprint: rub the uncoated side and see if it sheds fibers or leaves a powdery residue.
Conclusion
Choosing between paper, cloth, and film backings comes down to how the roll will be used on the shop floor. Paper is economical and works well for dry sanding and fine finishing, while cloth provides the tear resistance needed for aggressive stock removal or contoured surfaces. Film backings offer a uniform, flexible base that holds grit extremely evenly, which matters when you need a consistent scratch pattern. Grit consistency is not just a specification on a datasheet—it directly controls whether your finish shows random deep scratches or a clean, predictable surface. When you move to jumbo rolls, getting the width and length right from the start avoids awkward downtime. Always measure your machine's maximum roll capacity and consider the core size, because a slight mismatch can force you to rewind or trim material, adding labor cost that quietly eats into the quoted price.
Custom slitting can be a smart move if you regularly consume narrow widths that would otherwise create excessive trim waste, but it rarely pays off for standard sizes where stock rolls are already competitively priced. The hidden costs of low-priced rolls often show up later: weak splices that snap under tension, inconsistent backing thickness that causes chatter, or grit that sheds too early and forces you to replace the roll mid-job. A reliable OEM supplier will send you sample rolls for real-world testing, provide batch-to-batch consistency data, and answer technical questions without hesitation. Look for a partner who asks about your sanding pressure, workpiece material, and machine speed—not one who simply quotes the cheapest price per square meter. That kind of attention usually separates a supplier who understands jumbo roll performance from one who is just moving boxes.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn