Walk-Behind Power Trowel Manufacturing: Honest Concerns and What to Watch For
2026-10-04
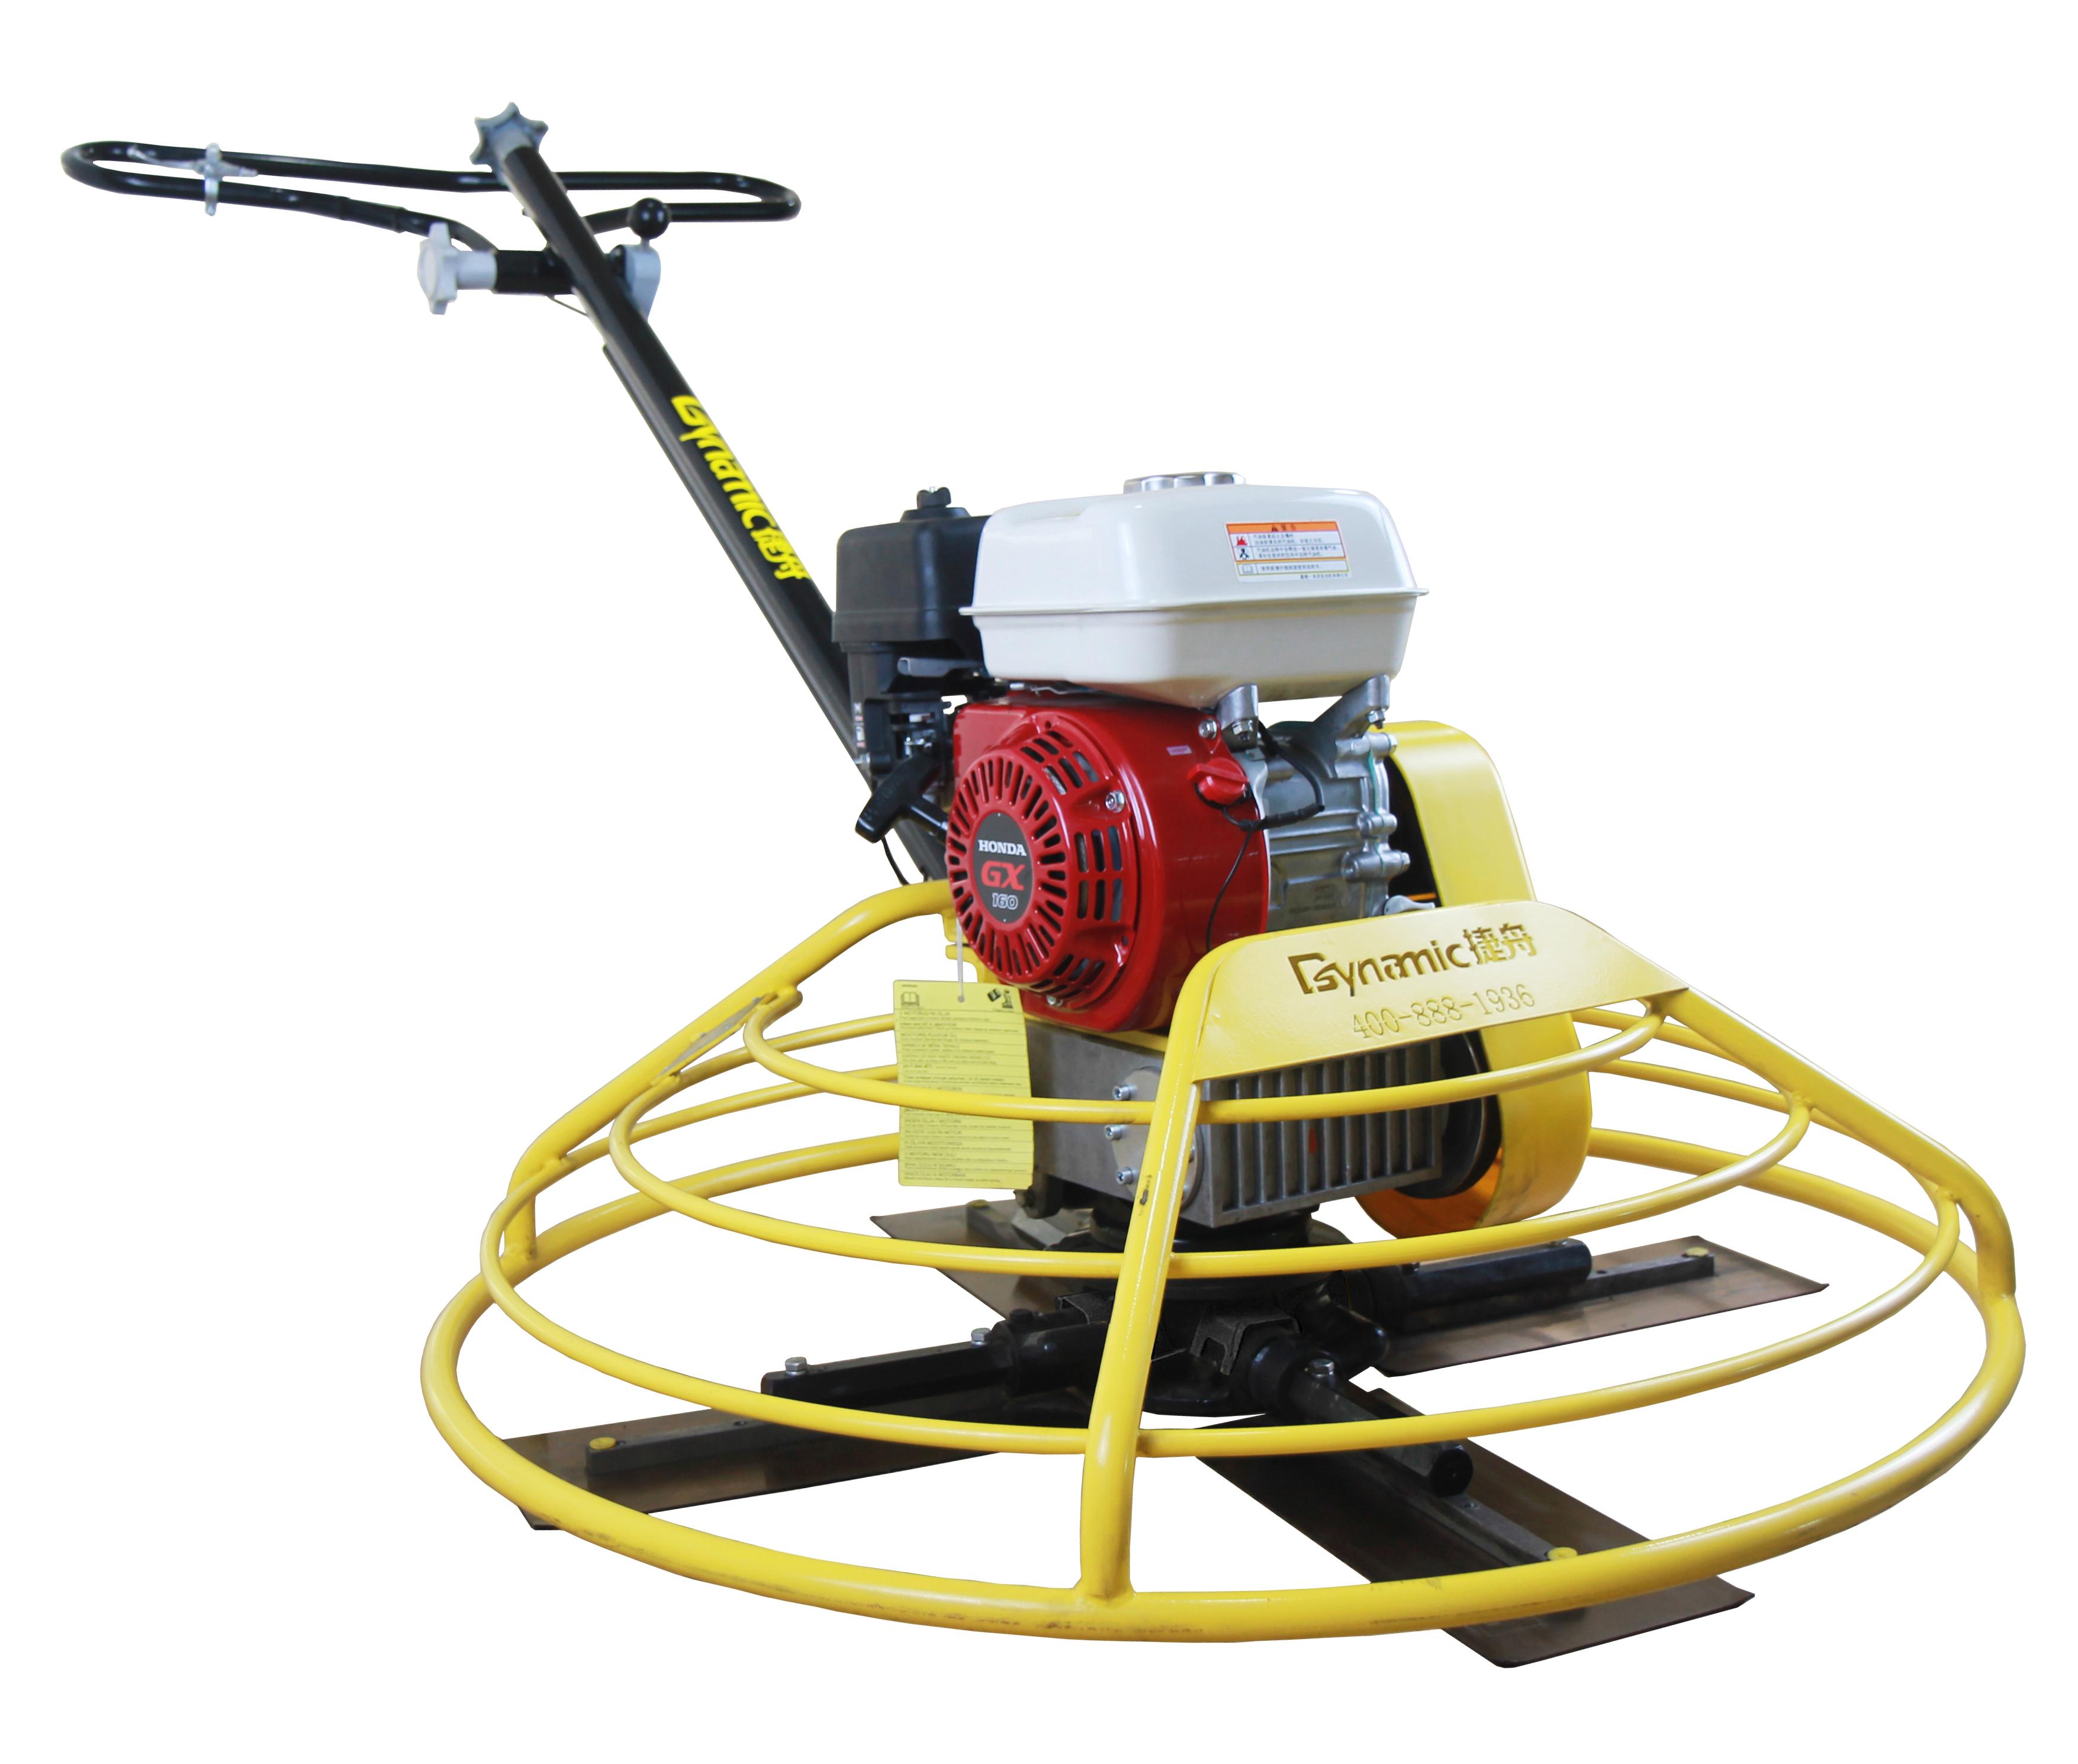
If you're in the market for a walk-behind power trowel, you've probably noticed that not all machines are built the same. From blade quality to engine reliability, the manufacturing choices behind these tools directly affect your concrete finishing results and long-term costs. Before you commit to a purchase, it's worth taking a hard look at what separates a dependable trowel from one that will let you down mid-pour. Brands like Dynamic have raised the bar in recent years, but honest concerns still remain across the industry. Here's what you need to watch for.
Casting Flaws You Can Spot Before the First Pour
A worn-out pattern leaves its fingerprints all over the sand before any metal ever flows. Look for rounded edges where sharp corners should be, or a slight taper on what was meant to be a straight wall. These are signs the pattern has been sanded, scraped, or repaired one too many times, and they translate directly into extra machining work later.
Core prints that don't sit flush with the mold cavity tell you something about core shift before you even set the core. Rock the pattern slightly on the molding board — if it teeters, the parting line isn't flat, and your casting will show a mismatch at that seam. You can also check the gating system drawn on the pattern: runners that narrow too quickly or sharp direction changes will cause turbulence, and that means trapped air and slag inclusions in the final part.
Shrinkage is predictable once you read the sections correctly. A boss that's three times thicker than the adjacent wall without a riser nearby is a guaranteed void waiting to happen. Look for isolated heavy sections that have no direct feed path — they'll pull liquid from the surrounding area as they solidify, leaving porosity you can't see until machining. These are failures cast into the geometry itself, not problems discovered after the pour.
Engine Hype Versus Real Torque on a Slab
Manufacturers love quoting peak torque figures as if they translate directly into thrust on every inch of tarmac. But when you actually roll onto a flat stretch of slab, the engine rarely sits in that narrow rpm window where the advertised maximum lives. Unless you keep the revs pinned near the redline, what you feel is a far more subdued machine.
The drivetrain gets in the way too. Clutch slip, gear ratio choices, and efficiency losses through a chain or shaft all shave away the raw torque leaving the crank. Add the grip limits of tires on smooth concrete, and the wheel torque becomes a distant cousin of the spec-sheet number.
The most honest approach is to ignore the peak figure and instead study the torque curve from idle to cruising rpm. An engine that delivers most of its twist at 3,000 rpm will feel more satisfying on a slab than one that needs to scream to 8,000 rpm before waking up, even if the latter posts prettier numbers on paper.
Blade Wear Patterns That Tell a Different Story
Most people assume a dull blade just needs sharpening, but the way the edge wears down often points to something else entirely. A polished strip along one side of the bevel doesn't come from normal cutting—it usually means the blade is deflecting under load or the workpiece is shifting mid-pass. If that strip runs the full length on only one face, the real problem may be a misaligned guide or an inconsistent feed angle rather than the steel itself.
Chips and micro-fractures clustered near the gullet tell a more specific story. When they appear on the trailing side of the tooth while the leading edge remains crisp, it's rarely a hardness issue. That pattern shows the material is being pulled away from the cut too quickly, creating a snapping force instead of a clean shear. Likewise, a blue or straw-colored band just behind the edge suggests heat buildup from friction, which can soften the temper long before the blade actually looks worn. Reading these signs early means replacing a $20 guide or adjusting speed instead of grinding away good steel.
Gearbox Longevity Under Daily Jobsite Abuse
On messy job sites, gearboxes rarely get the courtesy of clean oil and gentle starts. Operators jam levers, loads shift hard, and dust finds its way past seals that looked fine on the drawing board. The units that survive years of that treatment aren't built with magic alloys—they're built with heavier bearing preloads, thicker case ribs around the mounting face, and breathers placed where a pressure washer won't flood them. Those small decisions matter more than any spec sheet number.
Heat is the quiet killer most maintenance crews ignore. A gearbox can sit at 20% over its rated torque all morning without a single alarm, but the oil film thins and the backlash grows a little every hour. Eventually a ring gear tooth snaps not because it was weak, but because the housing had flexed enough to misalign the mesh. Good field longevity comes from keeping that flex under control and letting the oil drain heat away before it becomes a problem.
The real test is never a lab bench; it's a rented excavator in February with a rookie operator and a pile of frozen clay. If the gearbox can shrug off that kind of abuse—repeated shock loads, cold starts, and grit in every breather—then the design did something right. From the outside it just looks like another cast iron lump. On the inside, it's the difference between finishing the day or waiting for a flatbed.
Handle Vibration and the Cost of Ignoring It
When machinery starts to shake more than usual, it's not just an annoyance—it's a warning. Operators often get used to a certain level of buzz, but a sudden jump in vibration rarely fixes itself. Bearings wear faster, bolts loosen, and tiny cracks spread through housings before anyone notices. The real cost isn't the sensor you didn't buy; it's the unplanned downtime, the rushed replacement part, and the overtime labor that eats into the week's budget. A small imbalance today becomes a cracked frame next quarter.
Ignoring vibration doesn't make it disappear, it just moves the expense somewhere less convenient. Think of a pump that rattles for three weeks—then the coupling fails during a night shift. Now you're paying for an emergency crew, express shipping, and the lost production hours while the line sits still. Compare that to catching the imbalance early: a thirty-minute adjustment and a $20 set of shims. The math isn't complicated, but it's easy to postpone because the shaking feels tolerable. Tolerable, until it isn't.
Treat vibration as a message, not background noise. Walk the floor with a simple handheld meter, mark the machines that feel different, and track changes over time. You don't need a fancy dashboard or a cloud subscription. A notebook with monthly readings can reveal a trend months before failure. The cost of ignoring it is always higher than the cost of listening—whether that's a few minutes with a stethoscope or a proper accelerometer. What you pay for is the choice you make when the first shake appears.
The Certifications That Actually Survive a Site Inspection
Plenty of certificates look impressive until someone shows up unannounced and starts flipping through logbooks. The ones that survive a site inspection are rarely the fastest to obtain or the cheapest to maintain. They're built on records that match reality, employees who can answer questions without reaching for a script, and equipment that has obviously been maintained between audits, not just the week before.
During an inspection, the gap between a paper certification and a working one becomes obvious fast. Inspectors tend to look at the messy details: calibration dates, training sign-offs, corrective actions from past issues. A certification that holds up is one where those details are alive and current. For example, a food safety certificate means little if the temperature logs have gaps or the staff can't explain their allergen controls. The ones that pass are often backed by internal habits that make compliance the default, not a scramble.
What separates a reliable certification from a wall decoration is often follow-through. Certifications that survive inspections usually come with requirements for ongoing internal reviews, documented corrective actions, and management that treats nonconformities as fixes rather than failures. That kind of structure doesn't guarantee a perfect inspection, but it means problems are caught early and the evidence trail actually supports the certificate instead of contradicting it.
FAQ
Some units ship with poorly balanced blades, which cause vibration and uneven finishes. Gearbox leaks and throttle linkage failures also show up more often than they should, especially on budget models.
Look for thin stamped steel frames instead of cast or heavy-gauge components, plastic bushings where bronze or sealed bearings should be, and fasteners that rust quickly. A quick weight comparison with known quality brands often reveals a lot.
The gearbox should run cool and quiet. If the manufacturer uses splash lubrication with a poorly sealed housing, expect leaks and premature wear. Ask about bearing type and whether the gears are heat-treated; these details matter more than horsepower ratings.
For very light, infrequent work, maybe—but you still risk downtime and frustrating finishes. A mid-range unit from a maker with a real parts network often costs less over three years than a cheap model that needs blades, belts, and a gearbox rebuild.
Make sure the dead-man switch or operator presence control is robust and easy to reach. Watch for exposed belts or pulleys, weak blade guards, and throttle cables that can stick. Also confirm the handle folds without pinching fingers.
It's huge. Even well-built trowels need wear parts like blades, belts, and seals. If the manufacturer doesn't stock parts locally or ship quickly, a simple repair can leave you waiting weeks. Always ask where parts ship from and typical lead times.
Wobbling blades, inconsistent pitch adjustment, and a handle that flexes under load all hurt the finish. These often come from sloppy welding, poor blade balancing, or cheap pitch control mechanisms—not from operator error.
Yes, but the engine brand is only part of it. Even a good engine can be paired with a poor clutch or misaligned belt drive. Check that the engine mount is solid, the clutch engages smoothly, and the belt alignment doesn't cause premature wear.
Conclusion
Walk-behind power trowel manufacturing hides a lot of sins until the first pour reminds you. Casting flaws are the obvious ones—check for cold shuts, shrinkage cavities, or thin spots near bolt bosses before any concrete ever touches the blades. But a smooth body doesn't mean the engine delivers real torque on a slab. Plenty of spec sheets advertise peak horsepower that fades once the trowel hits wet concrete. Watch the blade pitch and how quickly it recovers under load; that tells you more than any dyno chart. Then there's the story in the wear patterns. If blades show uneven erosion or gouging after just a few jobs, the metallurgy or heat treatment wasn't up to standard—and that means early replacement costs.
Gearboxes are another quiet failure point. Daily jobsite abuse exposes weak seals, undersized bearings, and soft gear teeth that won't survive a season. You'll hear the whine or feel the heat before it locks up, but by then the pour is already lost. Handle vibration isn't just an annoyance—it's a direct line to operator fatigue, numbness, and long-term injury claims. If the handle transmits high-frequency buzz without dampening, the manufacturer cut corners on isolation mounts or balance. Finally, certifications matter only if they survive a real site inspection. Look for marks that match your local safety codes, not just glossy stickers. Ask for test reports, not marketing language. These honest concerns separate tools that last from ones that just look good in a catalog.
Contact Us
Contact Person: Annie
Email: [email protected]
Tel/WhatsApp: 8613391442963
Website: https://www.dynamic-eq.com